How to integrate filling & capping machines into cosmetic lines?
- How to sync filler speed with downstream capping machines?
- What layout best reduces contamination risk in cosmetic lines?
- How to validate dosing accuracy for viscous creams and lotions?
- What controls stopper orientation and cap torque consistency?
- How to integrate PLC networking between filler, capper, and ERP?
- Which changeover strategies minimize downtime for multiple SKU runs?
Article Title: How to integrate filling & capping machines into cosmetic lines?
Integrating a filling and capping machine into cosmetic production requires synchronized mechanics, validated dosing for viscous formulas, GMP-compliant layouts, PLC-to-MES connectivity, rapid changeover practices, and inline quality controls; this article gives practical engineering steps and standards to follow.
How to sync filler speed with downstream capping machines?
Start by establishing a master axis architecture: designate either the filler indexer or the primary conveyor as the servo-master and synchronize other axes with encoder feedback. Use precision encoders (incremental or absolute) and closed-loop servo drives to maintain phase alignment within a few degrees of encoder resolution; this prevents star-wheel misregistration and neck strikes common in rotary systems. For intermittent rotary fillers, set the filler cam profile to trigger product dispense only after cap presence or orientation sensors confirm chassis position. For continuous rotary or inline piston fillers, implement a phase-lock using the conveyor encoder so the capping turret receives bottles at consistent pitch. Include product-present photoeyes and pneumatic interlocks so high-speed fills pause automatically on capper jam. Finally, calibrate dynamic parameters under production load using the machine HMI recipe: acceleration, jerk limits, and torque margins to avoid bottle deformation, especially for PET and thin-wall containers.
What layout best reduces contamination risk in cosmetic lines?
Cosmetic production generally follows ISO 22716 Good Manufacturing Practices and cleanroom guidance from ISO 14644; typical non-sterile cosmetic areas aim for controlled environments equivalent to ISO Class 7–8 where airborne particulate control and unidirectional workflows reduce cross-contamination. Design the line with logical separation: raw material weighing and batching upstream, filling and capping in a dedicated area, and labeling/secondary packaging downstream. Use hygienic conveyors with minimal crevices, FDA/USP-compatible contact materials (316L stainless steel, PTFE where needed), and sloped surfaces for drainage. Implement positive airflow and separated maintenance access to avoid introducing contaminants during adjustments. Plan CIP or targeted local clean-in-place and validated manual clean protocols for nozzles and capping heads; document cleaning frequencies and swab test results in batch records. Add physical barriers and gowning zones where fragrance or preservative aerosols are present to protect product and operators.
How to validate dosing accuracy for viscous creams and lotions?
Select the proper metering technology first: piston fillers, progressive cavity (Moineau) pumps, and positive-displacement gear pumps are standard for high-viscosity formulations because they meter by volume with low shear. Validate dosing by running statistical process control: collect sample weights from a representative production run and calculate mean bias and standard deviation; acceptable tolerances depend on commercial agreements but aim for repeatability within +/-1 to 2 percent for finished weight on consumer cosmetics. Use inline checkweighers and install a reject station downstream to remove out-of-tolerance containers automatically. Monitor viscosity in the production environment with a representative lab viscometer (Brookfield or equivalent) and correlate viscosity shifts with dosing variance; adjust pump stroke, screw speed, or nozzle dwell accordingly. Maintain temperature control for thermosensitive lotions since small temperature changes alter viscosity and dispense volume. Keep recipe-controlled pump parameters in the PLC so changeovers restore validated dosing settings reliably.
What controls stopper orientation and cap torque consistency?
Cap alignment and torque are managed with a combination of mechanical guidance, capping head selection, and torque feedback. For screw caps, choose servomotor-driven capping heads that control torque and angle rather than simple slip-clutch designs; these provide programmable torque and torque-limiting profiles and can log torque values per bottle for traceability. For snap-on or press-fit closures, use a servo press with force and position feedback to ensure consistent seating without damaging the package. Add a downstream torque tester for sampled verification and an inline torque monitoring module if required for 100% inspection. Use vision systems to confirm cap orientation when appearance matters (logos, tamper bands) and integrate reject logic. Remember to specify torque units and acceptance ranges in the product specification sheet and validate with production sampling and a torque auditor device traceable to a national standard.
How to integrate PLC networking between filler, capper, and ERP?
Modern lines require layered integration. At the machine level, use industrial networks such as EtherNet/IP, PROFINET, EtherCAT or OPC UA for reliable deterministic communication between PLCs and drives; choose the protocol compatible with your control vendor. For higher-level integration, implement an MES layer that communicates with PLCs using OPC UA or standard API endpoints and maps to ERP for batch records, recipe distribution, and inventory updates. Follow ISA-95 principles to separate control, MES, and enterprise domains: keep real-time control inside the cell, while MES handles production scheduling, traceability, and quality events. Ensure recipes (filling volumes, torque limits, speed profiles) are version-controlled and downloadable from MES to PLC. Plan for cybersecurity: segregate networks, use VPNs for remote access, and apply role-based access control to avoid unauthorized recipe changes. Finally, include time-synchronized logging (NTP) and unique batch identifiers for every production run to satisfy traceability and recall preparedness.
Which changeover strategies minimize downtime for multiple SKU runs?
Adopt SMED principles and design changeover with modularity in mind. Use quick-change nozzles, interchangeable star-wheel pockets, and HMI-controlled recipe selection to reduce manual setup time. Standardize container pitch and neck finishes across as many SKUs as practical so mechanical adjustment ranges are minimized. Implement datum points and indexed fixtures for guides and chucks so operators can perform reproducible tool-less swaps in minutes. Create pre-staged SKU kits containing change parts, set-up sheets, and validated recipes to avoid on-line searching. Train operators on set-up and use pick lists in MES to guide each step and enforce checklists. Track changeover times and run root-cause analysis on frequent bottlenecks: ergonomics, part availability, or tool design. Investing in servo-assisted actuators and auto-guided format change capabilities will pay back in high-mix, low-volume cosmetic lines by reducing non-productive time dramatically.
Conclusion: Integrating filling and capping equipment into cosmetic lines is an engineering discipline combining mechanical synchronization, correct pump selection for rheology, contamination control consistent with ISO 22716, networked controls to MES/ERP using industry protocols, and operational practices that minimize changeover and maintain quality. Actionable short-term steps are: map product flows, choose the right metering technology, implement encoder-based synchronization, and ensure recipe-controlled PLC parameters with MES integration for traceability.
FULUKE brings practical cosmetic equipment know-how to implement these systems reliably, combining line-level engineering, control integration, and validation workflows to reduce downtime and ensure compliant production.
Contact us for a tailored quote at www.fulukemix.com or email flk09@gzflk.com.
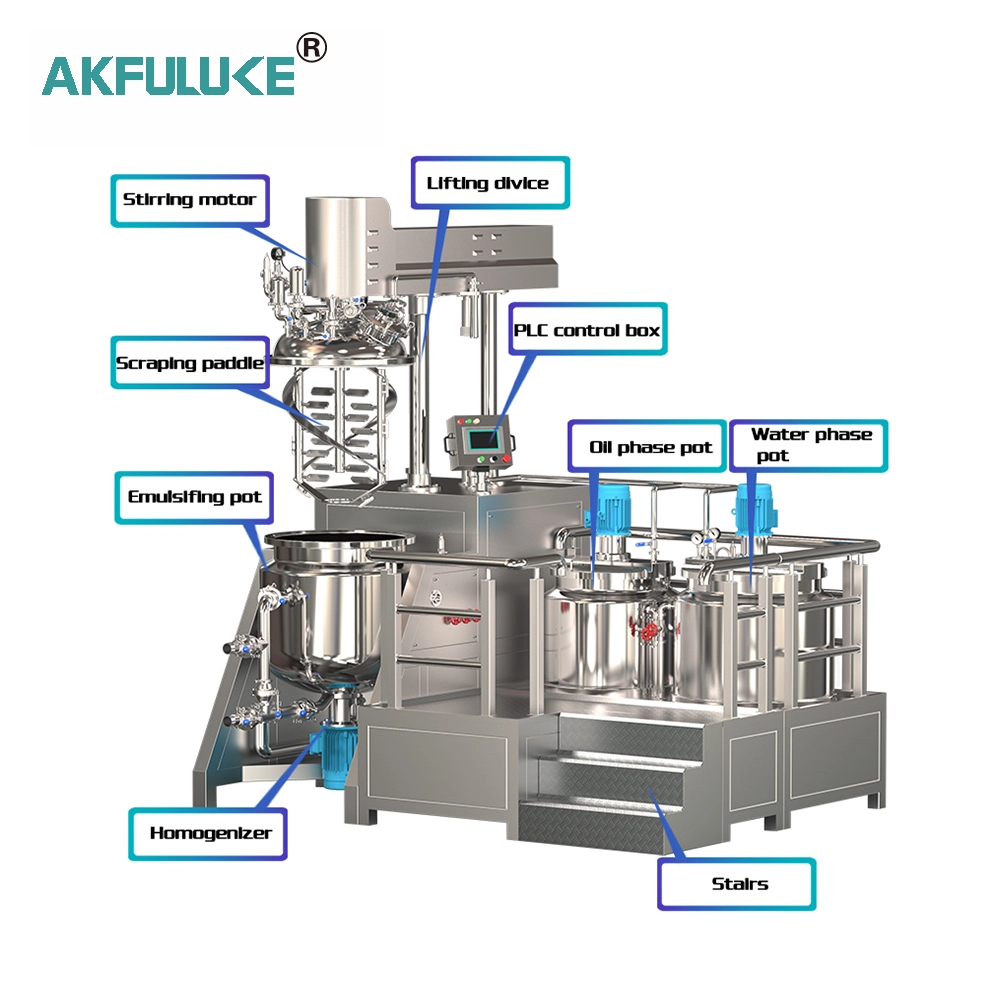
Application of Vacuum Emulsifiers in Cosmetics Production: How Are Creams, Lotions, and Serums Produced?
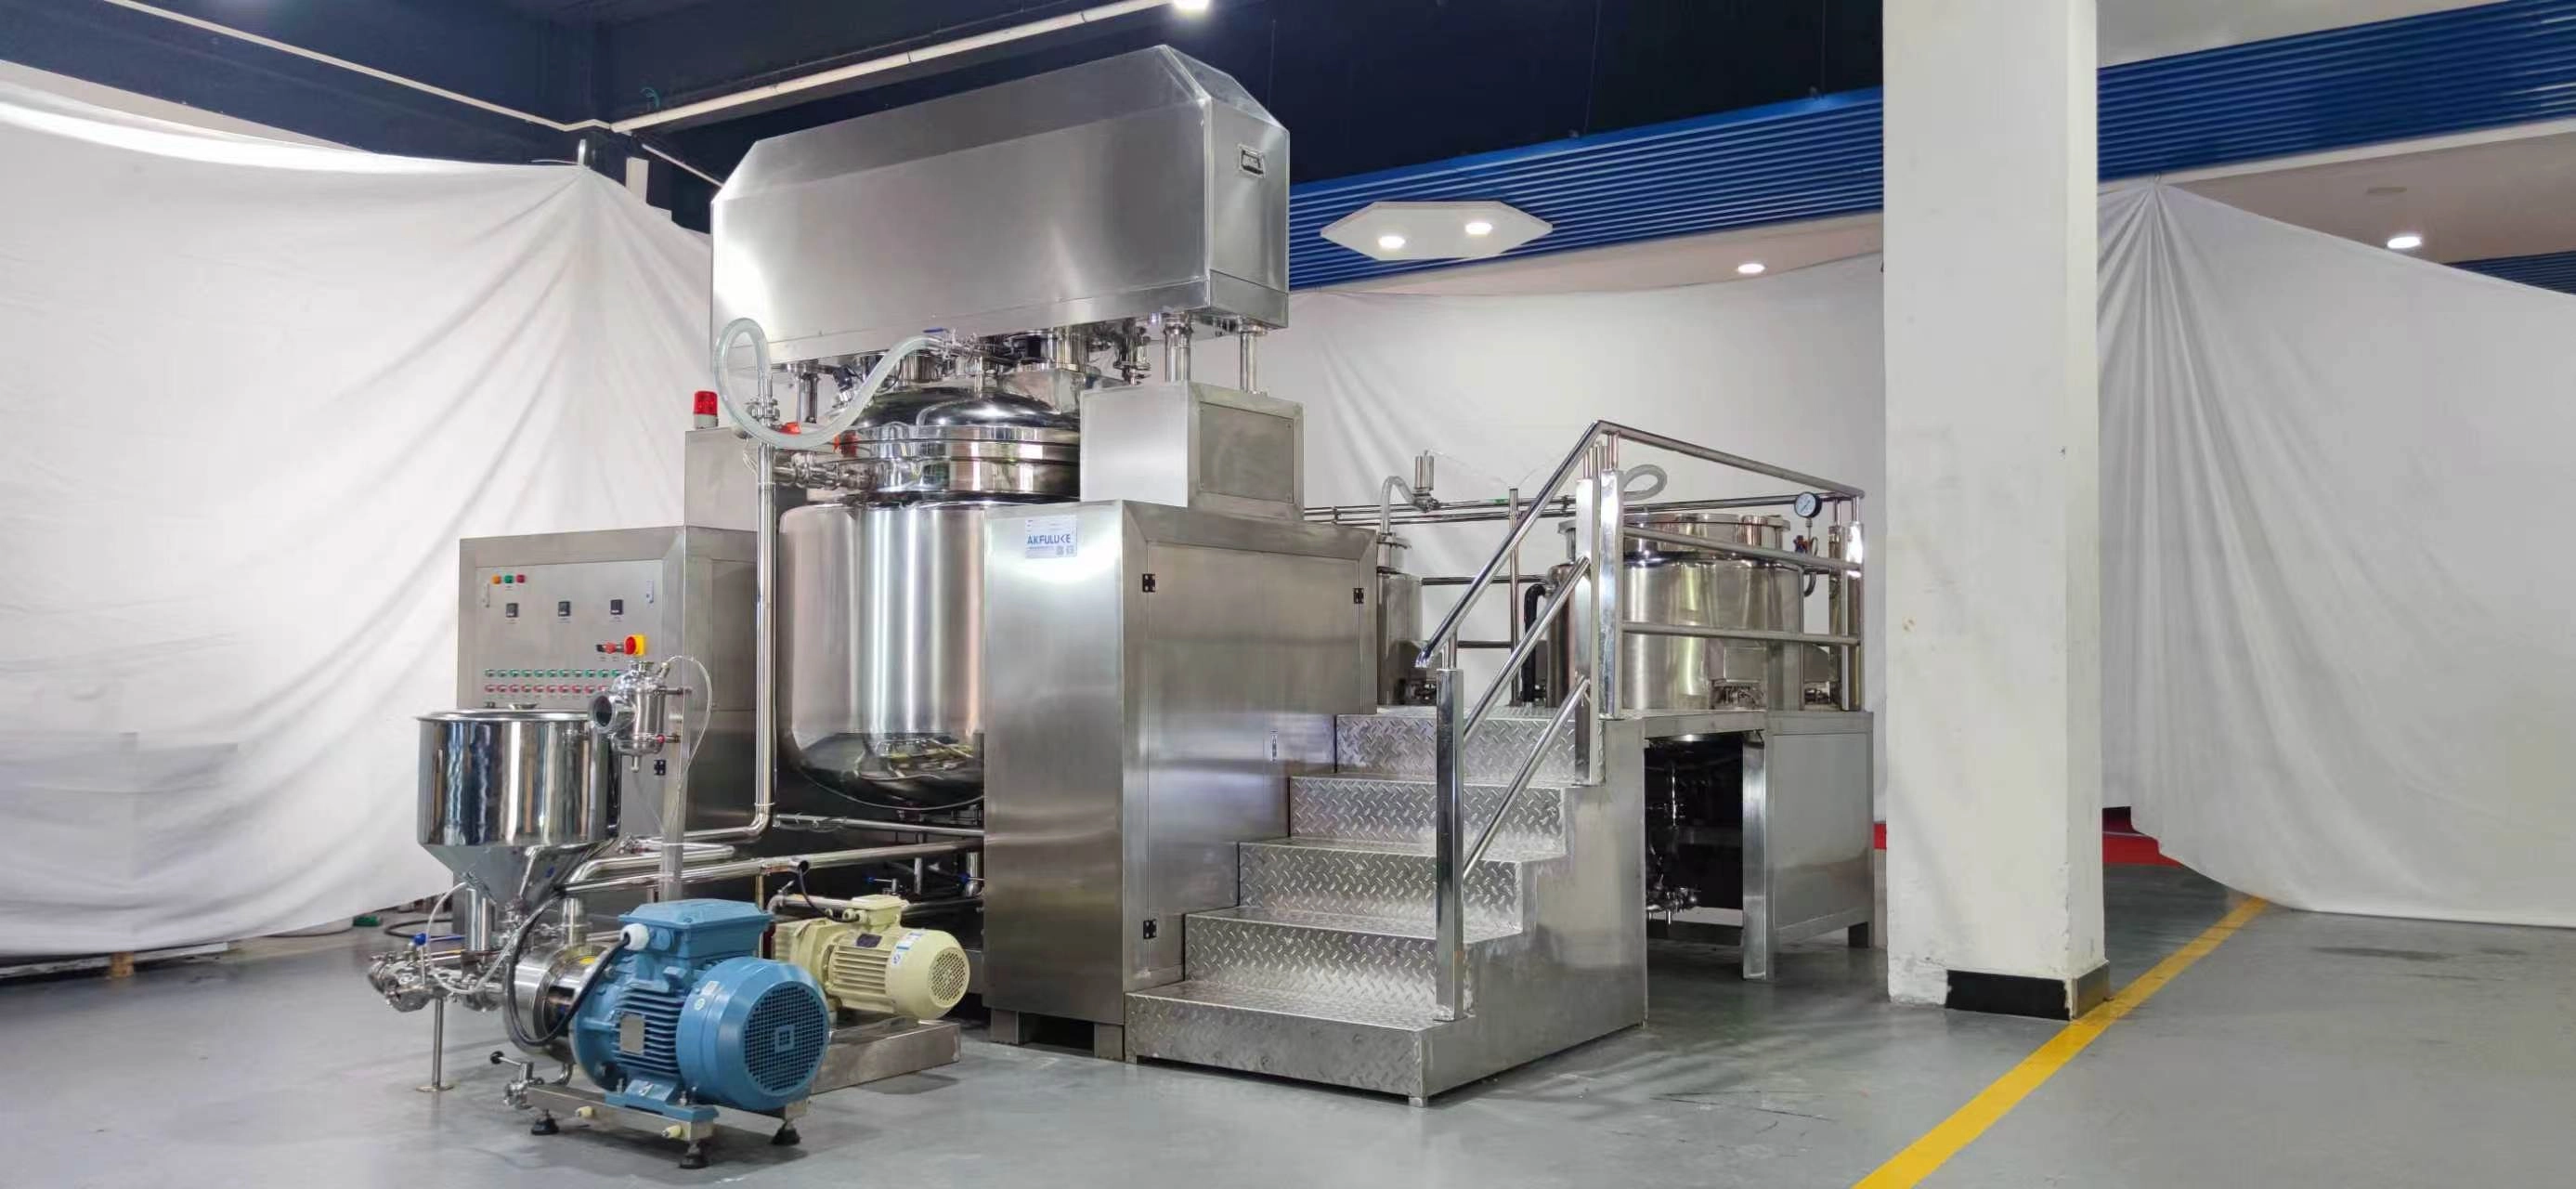
Should a vacuum emulsifier choose bottom homogenization or external circulation homogenization?
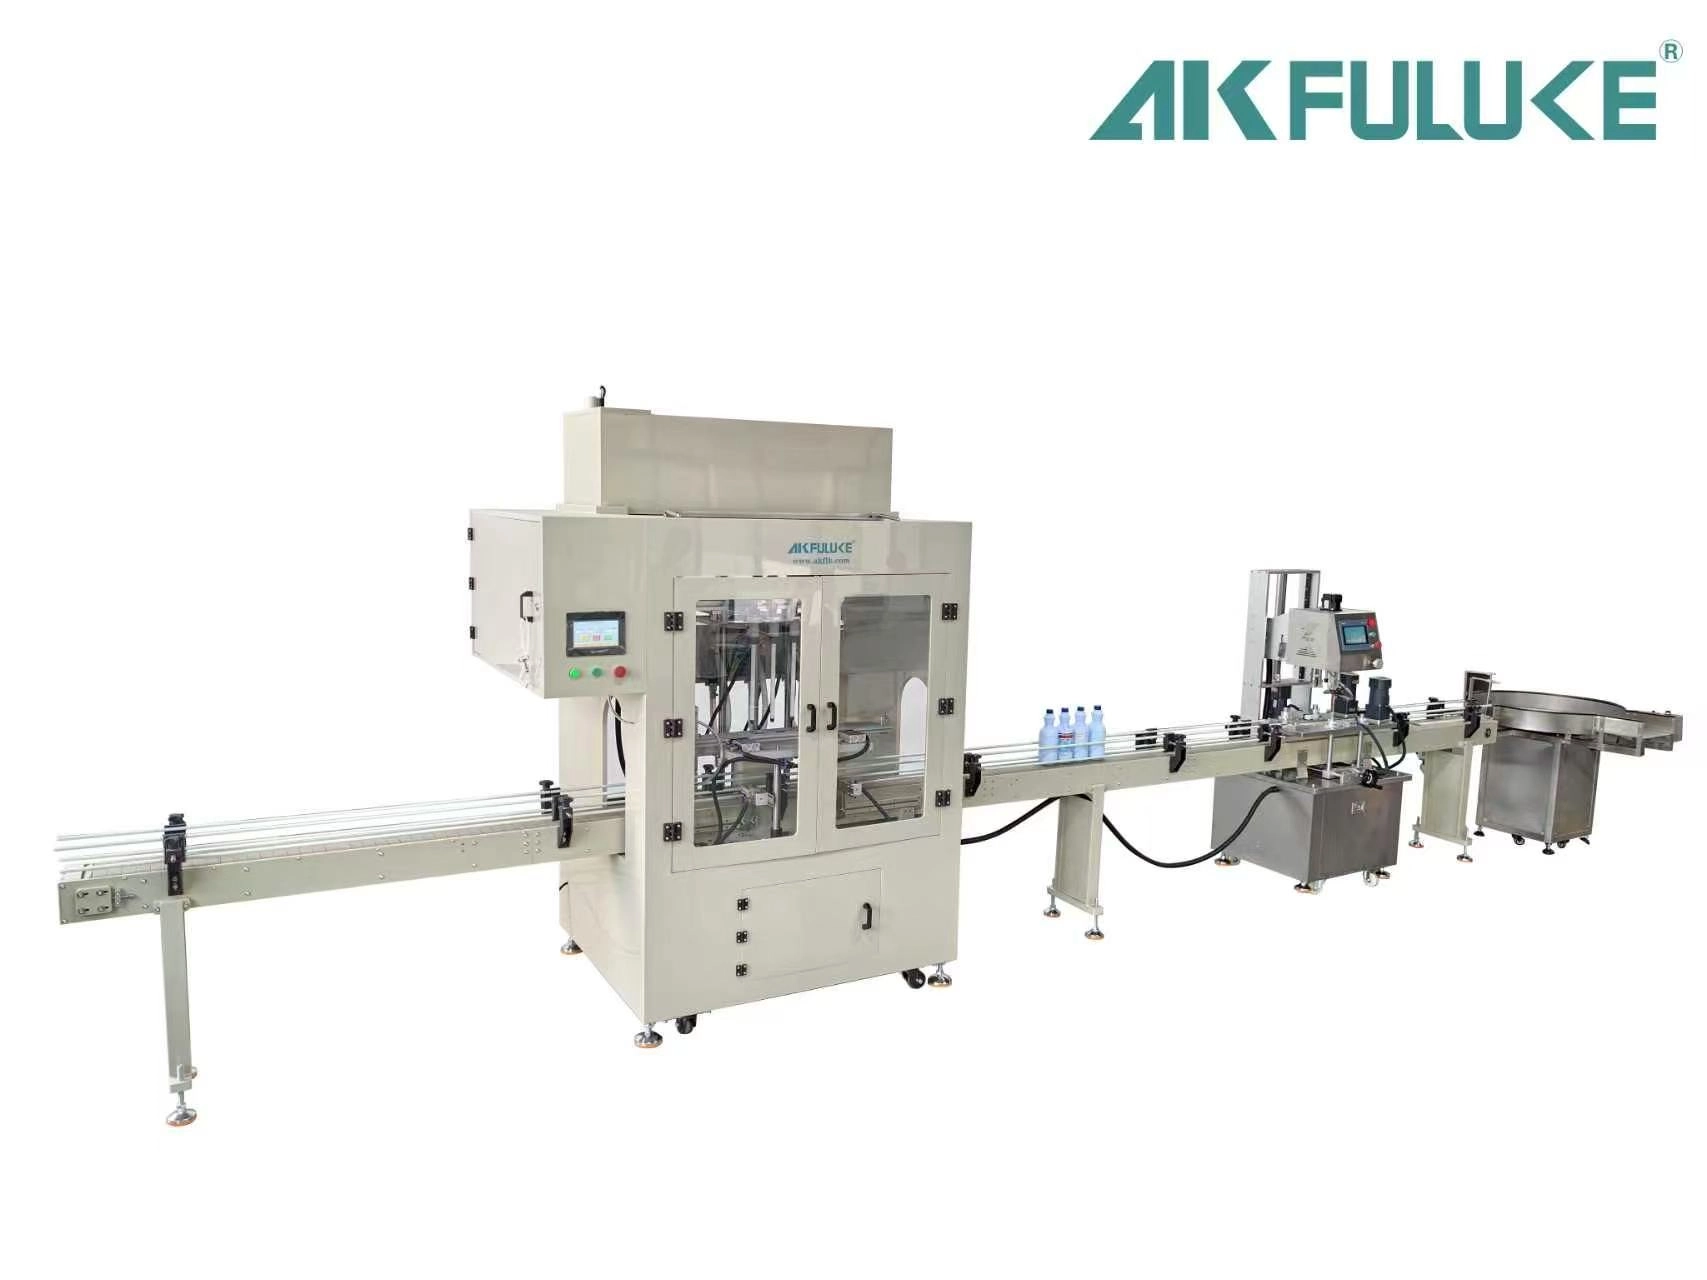
The ideal solution for filling corrosive liquids.

Case Study: New Clients from a Trade Show Visit an Existing Client's Cosmetics Factory—Leveraging Real Production Lines to Assist in New Factory Plan
Get in touch with FULUKE
If you have any comments or good suggestions, please leave us a message, later our professional staff will contact you as soon as possible.
You May Also Like
Automatic Acid Chemical Plastic Bottle Capping Anti Corrosion Bleach Filling Machine
Fixed Type Vacuum Mixing Emulsifying Equipment for Cosmetic Cream Ointment Lotion Vacuum Homogenizer Mixer
Automatic Labeling Machine Best Selling Automatic Tabletop Flat Surface Labeling Machine Round and Flat Bottle Automatic Labeler Machine
Storage Tank Mobile Fixed Chemical Liquid Storage Tank for Cosmetic, Perfume Food Grade Storage Tank Sealed Open Container
A leading manufacturer specializing in advanced machinery and complete production lines for the cosmetics, food, pharmaceutical, and chemical industries worldwide.
Contact FULUKE
Facebook
Instagram
YouTube